Leave Your Message
-
Phone
-
E-mail
-
Whatsapp
-
WeChat17782577059

Empowering pharmaceutical formulations, precision nutraceuticals, and preventive clinical nutrition with high-potency standardized botanical extracts, active metabolites, and turnkey OEM/ODM bio-manufacturing.
Direct factory supply of high-purity extracts and nutritional substrates engineered for specialized dietary formulations, pharmaceutical intermediate synthesis, and health beverage matrices.

The intersection of pharmaceutical engineering and nutritional science is reshaping global preventive health, creating a multi-billion dollar market for standardized botanical and active metabolites.
Global healthcare paradigms are transitioning from acute reactive treatment to long-term proactive prophylactic intervention. Functional food ingredients bridge this gap by delivering clinically proven bioactive markers that modulate biochemical pathways without pharmaceutical side effects, making them vital in integrative disease management.
Cutting-edge bio-fractionation, liposomal nano-encapsulation, and enzymatic fermentation are unlocking unprecedented bioavailability. Manufacturers utilize computational metabolomics and molecular docking simulations to synergize botanical co-factors, maximizing the target tissue delivery of polyphenols, peptides, and organic acids.
With authorities worldwide enforcing stringent cGMP, FSSC22000, and FDA dietary compliance, functional food ingredients must adhere to pharmaceutical-grade documentation. Complete batch traceability, heavy metal containment, pesticide residue clearance, and standardized potency assays are non-negotiable standards.
Targeted therapeutic categories where functional food ingredients act as active primary ingredients or complementary therapeutic co-factors.
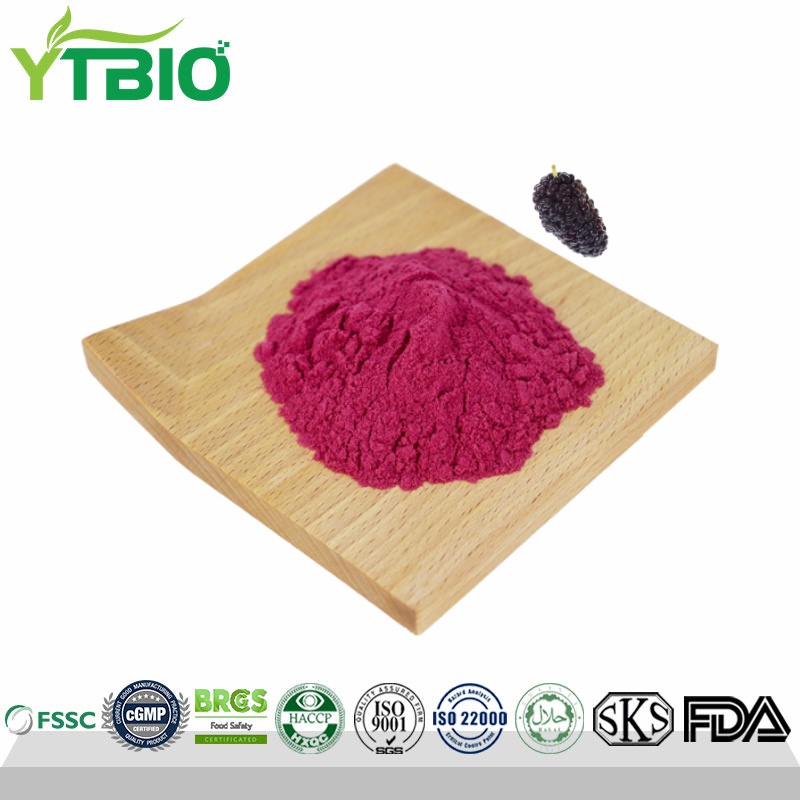
Standardized plant extracts such as Mulberry Extract (rich in 1-Deoxynojirimycin / 1-DNJ) effectively inhibit alpha-glucosidase enzymes in the brush border of the small intestine. This blunts postprandial glucose surges, enhances insulin sensitivity, and provides nutritional support for type-2 diabetes management, metabolic syndrome therapies, and medical weight management formulas.
Functional derivatives like N-Acetyl-L-Glutamine serve as essential fuel substrates for enterocytes, accelerating mucosal barrier repair and reducing intestinal hyperpermeability ("leaky gut"). Combined with organic acids (Lactic Acid, Citric Acid) that regulate lumen pH, they foster an optimal milieu for probiotic colonization and suppress opportunistic pathogen proliferation.
Marine-derived lipids such as Bulk Green-Lipped Mussel Oil provide a rare spectrum of ETA (Eicosatetraenoic Acid), EPA, and DHA. These marine polyunsaturated fatty acids downregulate 5-lipoxygenase (5-LOX) and cyclooxygenase-2 (COX-2) enzymatic cascades, alleviating chronic synovial inflammation, joint degeneration, and osteoarthritis discomfort without gastrointestinal toxicity.
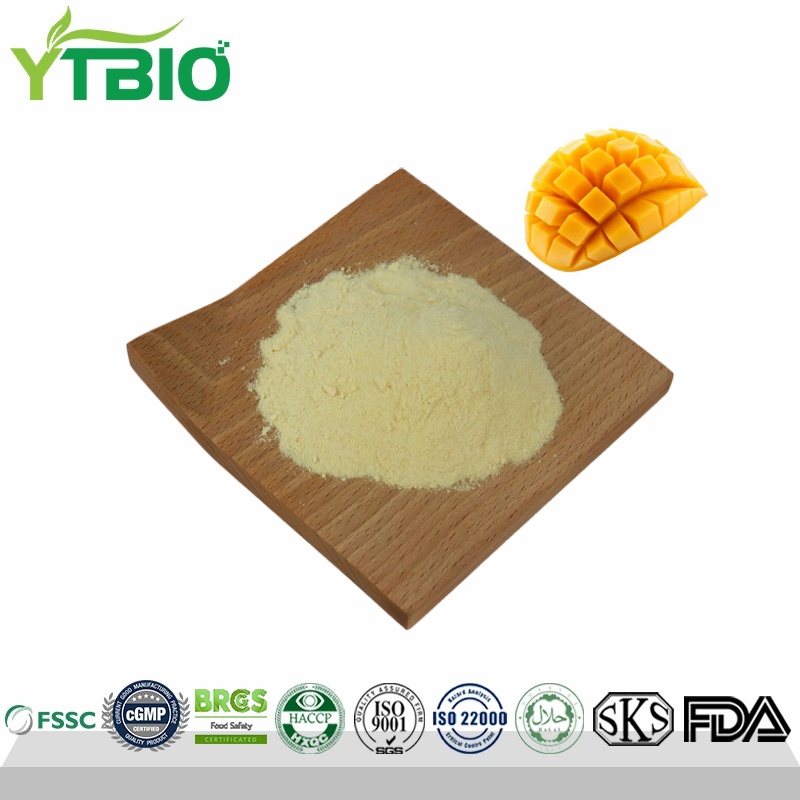
Micro-milled fruit powders (Kiwi, Mango, Mulberry) supply high-density flavonoids, ascorbic acid derivatives, and carotenoids. These botanical co-factors neutralize reactive oxygen species (ROS), protect neuronal mitochondrial membranes against oxidative damage, and support neuro-vascular microcirculation in cognitive vitality and healthy aging formulations.

Shaanxi Yuantai Biological Technology Co., Ltd. was established in 2014. Its headquarters is located in Xi'an and its modern factory is located in Weinan Economic and Technological Development Zone. The factory covers an area of 10000+㎡.
At present, the company's main categories include: capsules, granules, tablets, solid beverages, soft candies and other OEM categories. YTBIO has 10 years of production experience in the raw material field. The main categories include: herbal extracts, nutritional supplements, organic extract raw materials and cosmetic raw materials.
YTBIO is a comprehensive health food manufacturer. With its deep understanding of the raw material industry and botanical actives, it uses decade-long industry experience to provide compounding solutions from raw materials to finished products, supporting professional turn-key solutions in product packaging, flexible application of ingredients, and custom product label design. In addition, we are continuously committed to developing new products to provide customers with more product and formula options to meet diverse international market demands.


To ensure product quality and production process standards, we have passed cGMP, FSSC22000, BRC, HACCP, ISO9001, ISO22000, HALAL, KOSHER, FDA, and EU & US organic certifications.


OEM Categories: Capsules, Granules, Tablets, Solid Beverages, Soft Candies, and Custom Formulas.
OEM Content: Raw materials sourcing, formula design, encapsulation, packaging, and custom label compliance.

Regarding capsules, we are able to provide finished packaging or standalone operation production, such as:
We provide a comprehensive selection of shell options to match dietary, religious, and release profile requirements:


End-to-end tableting solutions from wet granulation and direct compression to film and enteric coating:
Within our solid beverage production facilities we are able to offer the production of instant herbal teas, functional granular beverages, and pack them directly into finished consumer units:

We utilize the highest quality botanical and marine raw materials from reliable certified suppliers, producing and processing directly in our own facility. Providing a comprehensive one-stop service from solvent extraction, ultra-filtration, spray drying, and enzymatic refining to final consumer delivery.
Explore our full spectrum of food-grade and pharmaceutical intermediate raw materials ready for global bulk export and custom OEM contract manufacturing.