Leave Your Message


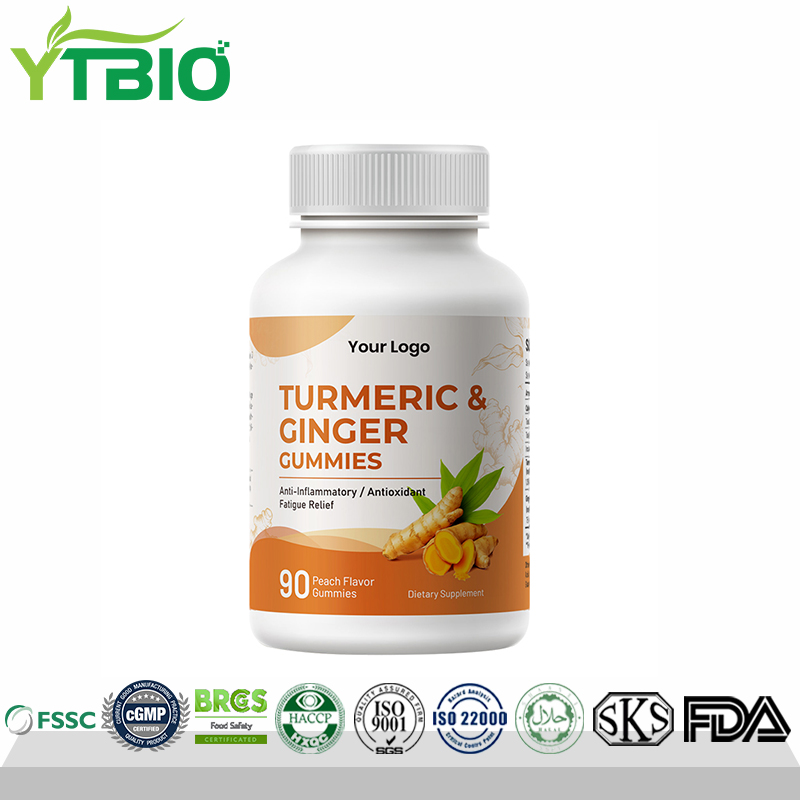
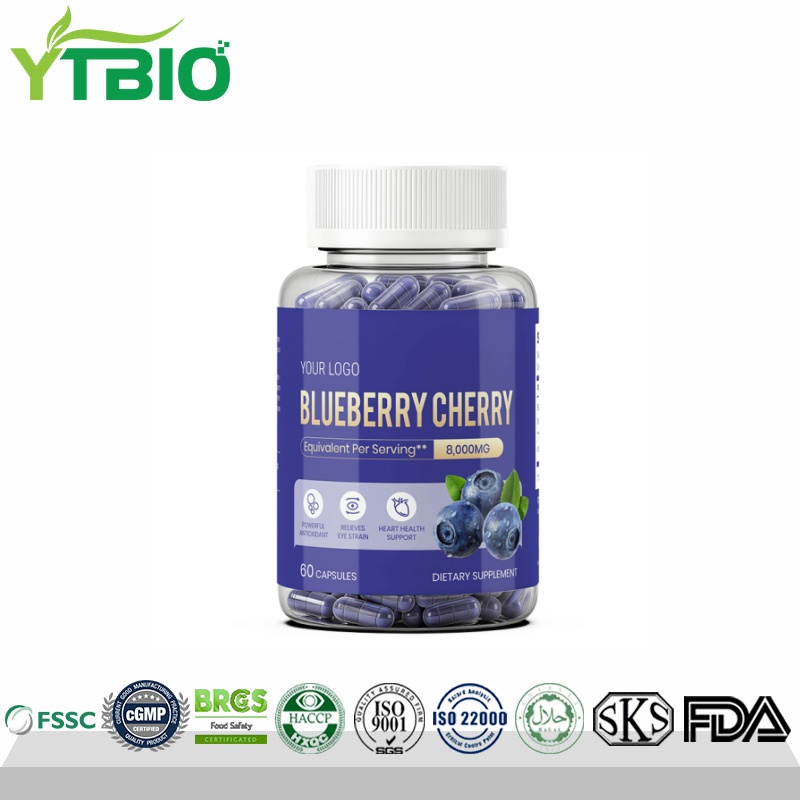
In the modern health and wellness landscape, immune support is no longer a seasonal consideration. It has evolved into a year-round, proactive lifestyle choice for consumers worldwide. As global markets witness a surge in health consciousness, dietary supplement brands are seeking reliable, scalable, and innovative manufacturing solutions. This is where a specialized tablet OEM manufacturer for immune support becomes a critical strategic partner.
The manufacturing of immune support tablets requires a deep understanding of nutritional science, raw material stability, and high-precision machinery. The active ingredients commonly used to boost the immune system—such as Vitamin C, Zinc, Elderberry, Turmeric, Ginger, and various herbal extracts—are often sensitive to environmental factors like heat, moisture, and compression pressure. A state-of-the-art OEM manufacturer utilizes advanced tableting technologies to preserve the bioactivity of these compounds, ensuring that the end consumer receives a product that is both effective and safe.
The dietary supplement market has experienced a significant paradigm shift. The global immune support supplements market size was valued at billions of USD and is projected to expand at a compound annual growth rate (CAGR) of over 7% in the coming years. Consumers are increasingly favoring convenient solid dosage forms, with tablets remaining one of the most trusted and widely consumed formats due to their ease of storage, precise dosage control, and long shelf life.
Furthermore, clean label demands are pushing manufacturers to innovate. Brands now require tablets free from synthetic binders, artificial colors, and unnecessary excipients. Modern tablet OEM facilities are responding by developing organic-compliant tableting processes, utilizing natural excipients like organic acacia gum, rice concentrate, and plant-based coatings. This alignment with consumer values is crucial for brands looking to establish authority in the premium health market.
We specialize in synergistic immune blends combining vitamins, minerals, and standardized botanical extracts. Our 50+ R&D team customizes tablet size, shape, and release profiles to match your brand requirements.
Utilizing high-speed rotary tablet presses, boiling granulation, direct compression, and advanced film coating. We resolve challenges related to hygroscopic herbal powders and low-compressibility actives.
Operating under strict cGMP guidelines. Every batch of raw materials and finished tablets undergoes comprehensive testing for purity, potency, heavy metals, and microbiological safety.
Immune health is not a one-size-fits-all concept. Modern consumer segments require targeted formulations that address specific lifestyle needs. A professional tablet OEM manufacturer can assist brands in developing customized formulations for various target demographics:
To meet these diverse application scenarios, OEM manufacturers must possess a versatile raw material supply chain and advanced processing technology. For example, processing botanical powders like turmeric or ginger requires precise moisture control during the granulation phase to prevent clumping and maintain the active curcuminoid and gingerol content.
The efficacy of an immune support tablet depends heavily on its disintegration and dissolution rates. If a tablet is compressed too tightly, it may pass through the digestive system without releasing its active ingredients. Conversely, if it is too loose, it will crumble during transport. OEM manufacturers solve this by optimizing the binder-to-active ratio and using specialized disintegrants that allow the tablet to break down efficiently in the stomach or intestines.
Enteric and film coating technologies are also employed to protect sensitive ingredients from stomach acid, allowing them to be absorbed in the small intestine for maximum bioavailability. Coatings also play a crucial role in masking the bitter tastes or strong odors of certain natural botanicals, thereby improving consumer compliance.


Nutritional supplement raw materials are mainly used in the fields of medicine, health products, etc. to supplement the amino acids, trace elements, vitamins, minerals, etc. required by the human body.
YTBIO has ten years of experience in the raw materials industry and has sufficient understanding of the industry and products. Now we support OEM/ODM services. Through continuous innovation and persistence in quality, we are committed to providing reliable health products to global customers and promoting the sustainable development of the health industry.
See More

The capsule categories we provide are: hard capsules, soft capsules, and pellet capsules.
About customization: ingredients, packaging, labels, etc. can all be customized. In addition, we focus on customized formulas, and a variety of existing formulas and stocks are waiting for you to choose. The production facilities and equipment meet national standards, and the production process is strictly carried out in accordance with GMP requirements.
See More

Technologies include boiling granulation, direct tablet compression of all powders, semi-film coating, new excipients, new processes and production linkage, etc. The production materials meet national standards, undergo comprehensive inspection and quality control, and the production process is strictly carried out in accordance with scientific production process.
About customization: ingredients, shape, packaging, labeling, etc. In addition, there are many formulas and stocks for you to choose from.
See More
Since its establishment in 2014, Shaanxi Yuantai Biological Technology Co., Ltd. has always focused on the research, development, production and sales of herbal extracts, nutritional supplements, organic products and OEM/ODM services.
With high standards of product quality and a professional team as the core, the company provides customers with high-quality health product solutions. It always adheres to the concept of sustainability, balance and health to ensure that the products meet market demand and consumer expectations.

All YTBIO products are produced by ourselves, covering an area of 10000+ square meters, with advanced extraction equipment and mature extraction technology. In addition, we have also set up separate production areas for capsules, granules, tablets, solid beverages, etc.

The production facilities and equipment meet national standards, and the production process is strictly carried out in accordance with GMP requirements. And constantly update QA/QC standards to enhance the core competitiveness in quality control and R&D levels.

The certificates currently obtained include cGMP, FSSC22000, BRC, HACCP, ISO9001, ISO22000, HALAL, KOSHER, FDA, organic and other globally recognized credentials.
As the supplement industry embraces Industry 4.0, the role of a tablet OEM manufacturer is evolving from a simple contract processor to an integrated technology partner. Artificial Intelligence (AI) and data analytics are beginning to play significant roles in formulation design, predictive shelf-life stability modeling, and supply chain optimization.
AI-driven tools analyze massive databases of clinical trials and nutritional studies to identify synergistic combinations of immune-supporting compounds. For instance, determining the precise ratio of polyphenols in blueberry extract and active curcuminoids in turmeric that maximizes cellular anti-inflammatory responses is now done using computational modeling. This reduces formulation trial-and-error, accelerating time-to-market for new brands.
In manufacturing, smart sensors on rotary tablet presses monitor compression force, weight uniformity, and tablet thickness in real-time. Any deviation is immediately corrected by automated feedback loops, minimizing waste and ensuring that every single tablet meets therapeutic grade standards. This level of quality control is especially critical for brands targeting the clinical and practitioner channels, where dosage accuracy is paramount.
Another major trend shaping the future of supplement manufacturing is sustainability. Consumers are highly conscious of the environmental impact of plastic bottles. Leading OEM manufacturers are actively developing sustainable packaging solutions, including biodegradable tablet bottles, compostable pouches, and refillable glass container systems.
Additionally, green chemistry and eco-friendly extraction methods (such as supercritical CO2 extraction and water-based processing) are being used to obtain raw materials. This ensures that the active botanicals used in immune support tablets are not only effective but also sustainably and ethically sourced, preserving the planet's resources for future generations.
Provide customers with quality products.
For product information and quotes, contact us today!


